Skip to content

2026 Top Pallet Conveyor Types for Global Buyers?

For global buyers, selecting the right Pallet Conveyor in 2026 means examining more than transport speed. Warehouse layouts, pallet materials, load weight, climate, and automation goals all influence the correct design. A steel pallet carrying 1,000 kilograms needs different support than a lightweight plastic pallet. It depends.

This guide introduces the main pallet conveyor types used in distribution centers, factories, cold stores, and fulfillment operations. Roller conveyors suit many standard loads and can support accumulation zones. Chain conveyors handle challenging pallet bases and frequent transfers. Belt-driven rollers offer controlled movement, while turntables, lifts, and transfer cars connect different directions or elevations. Each option has practical strengths. Each also has limits.

Experienced buyers should evaluate frame construction, roller spacing, motor capacity, controls, guarding, noise, and maintenance access. A reliable system must fit existing equipment, not only perform well in a demonstration. Ask suppliers for load calculations, layout drawings, service plans, and documented performance data. Check how replacement parts will reach your facility. That detail is often overlooked.

Total cost matters. Purchase price is only one part of ownership. Energy use, downtime, cleaning, operator training, and spare components can change the final result. Local technical support may matter more than a small discount. Site measurements must be accurate. Measure twice.

The following overview compares leading Pallet Conveyor types for international buyers. It also highlights suitable applications, selection concerns, and design mistakes worth reconsidering before approval. No single conveyor wins every project. Good decisions come from matching proven engineering with real operating conditions.

2026 Top Pallet Conveyor Types for Global Buyers?

What Is a Pallet Conveyor and How Does It Work?

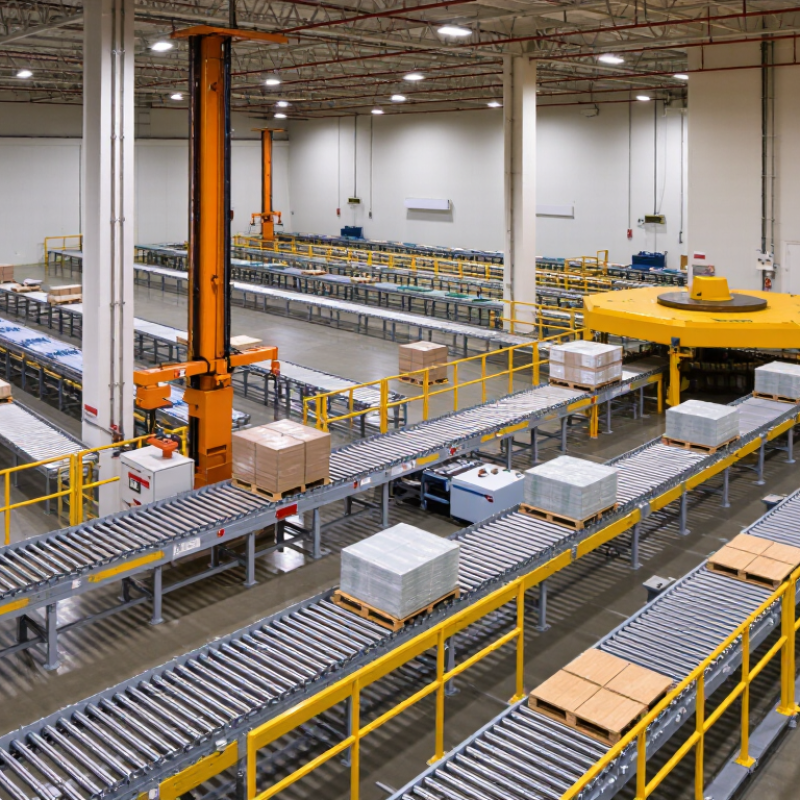
A pallet conveyor is a powered or gravity-driven system that moves loaded pallets between storage, production, and shipping areas. It uses rollers, chains, belts, or a combination of these parts. The best choice depends on pallet weight, dimensions, speed, and handling conditions.

In practical warehouse commissioning, powered roller conveyors are common for steady transport. Chain conveyors can move heavy pallets with uneven bases. Gravity roller sections often support short transfers and buffer zones. Sensors detect pallet positions and control starting, stopping, and spacing. A drive motor turns the rollers, while side guides keep the load aligned. Transfer units can shift pallets between conveyor lines. Simple equipment is often more reliable, although it may use more floor space. That trade-off deserves careful review.

Tips: Measure the heaviest pallet first. Check its bottom structure, not only its length and width. Leave access for cleaning and maintenance. Ask for load tests with real pallets. A specification sheet may look perfect, but field conditions can differ. Humidity, dust, and frequent stops can change performance. Also confirm local electrical requirements and safety expectations before ordering. Mistakes happen when buyers focus only on speed. A slower, stable line may serve better than a fast system with frequent jams.

2026 Top Pallet Conveyor Types for Global Buyers

A pallet conveyor is a material-handling system that moves loaded pallets between storage, production, picking, and shipping areas. Powered rollers, chains, belts, transfer cars, and turntables are selected according to pallet weight, surface condition, routing complexity, and required throughput.

The chart compares representative maximum pallet-load ratings commonly used in industrial conveyor designs. Actual capacity depends on pallet dimensions, load distribution, conveyor length, frame construction, drive configuration, and safety factors.

Core Pallet Conveyor Types for Global Buyers in 2026

Pallet conveyors in 2026 are becoming more modular, measurable, and easier to maintain. Global buyers usually compare chain-driven roller, belt, and powered roller conveyors for core transport tasks. Chain-driven rollers handle heavy pallets and uneven loads with dependable traction. They suit warehouses moving steel containers, boxed machinery, or stacked cartons. Powered rollers offer smoother movement and flexible zone control. They work well when pallets require controlled spacing near picking or wrapping stations. Belt conveyors provide continuous support for unstable loads, although belt tension and surface wear need regular inspection.

Transfers, turntables, and pallet lifts connect the main conveyor routes. A transfer unit moves pallets between parallel lines without manual handling. Turntables change pallet direction in compact spaces. Lifts serve multiple levels, but their safety sensors and load ratings require careful verification. My practical preference is to test a loaded pallet during peak operating conditions, not only during commissioning. A quiet empty conveyor can hide vibration, skewing, or delayed stopping. It is easy to overestimate capacity. Actual performance depends on pallet quality, moisture, temperature, and operator habits. Buyers should request maintenance access, spare-part availability, electrical compatibility, and documented safety testing. Local technicians may also need clear training materials. The cheapest layout is not always the most reliable one. That lesson remains uncomfortable, but useful.

How to Match Conveyor Types to Pallet Loads and Workflows

Selecting a pallet conveyor begins with the load, not the floor plan. Powered roller conveyors suit pallets with firm, continuous bottom surfaces. Chain conveyors handle uneven bases and heavier loads more confidently. A damaged pallet may still move, but it can create costly jams.

Check pallet weight, length, width, underside openings, and center of gravity. For mixed loads, use adjustable guides and controlled accumulation zones. A transfer unit helps change direction without manual handling. Turntables save space, but they need accurate stopping and enough clearance. For repetitive, high-volume routes, shuttle systems can reduce travel between storage lanes and workstations.

MHI’s 2024 Annual Industry Report found that 43% of supply chain leaders planned to increase technology investment. That figure supports automation, but it does not justify buying the most complex conveyor. The workflow matters more. A short line with frequent picking needs gentle accumulation and clear access. A long line feeding palletizing equipment needs stable speed, sensors, and reliable load spacing.

Test real pallets, not ideal samples. Dirt matters. Forklift impacts matter too. I have seen layouts fail because a “standard” pallet was not standard at all. Capacity calculations should include peak hours, damaged pallets, maintenance stops, and future load changes. A conveyor that works perfectly today may become restrictive after one product-size change. Reliability often comes from simpler equipment, better controls, and honest site measurements.

(MHI, 2024 Annual Industry Report)

2026 Top Pallet Conveyor Types for Global Buyers? – How to Match Conveyor Types to Pallet Loads and Workflows
Conveyor Type Typical Pallet Load Compatible Pallet Characteristics Best-Fit Workflow Typical Applications Main Advantages Key Limitations Important Selection Criteria
Powered Roller Conveyor Approximately 300–2,000 kg per pallet, depending on roller size, frame design, and drive arrangement Rigid pallet base Flat underside Wood, plastic, or steel pallets Straight-line transport, accumulation, pallet staging, and integration with scanners or automated storage systems Receiving, production lines, pallet buffer zones, order consolidation, and shipping areas Versatile layout options; supports accumulation; suitable for moderate to high throughput; easy to integrate with sensors and controls Requires adequate pallet contact with the rollers; uneven or damaged pallet bottoms may cause poor movement or instability Load weight, pallet bottom design, roller pitch, accumulation method, conveyor speed, and required stopping accuracy
Chain Conveyor Approximately 500–3,000 kg per pallet, subject to chain arrangement and equipment design Strong runners Open pallet underside Rigid or reinforced pallets Heavy-duty transfer, pallet movement through demanding production areas, and applications requiring positive engagement Automotive components, metal products, bulk materials, heavy manufacturing, and pallet transfer stations High load capacity; reliable positive drive; handles some pallet surfaces that are less suitable for standard rollers Usually less suitable for smooth accumulation; can be noisier; chain maintenance and guarding are important Number and spacing of chains, pallet runner position, load distribution, impact loading, lubrication, and guarding requirements
Belt Pallet Conveyor Approximately 100–1,500 kg per pallet, depending on belt width, belt construction, and drive capacity Flat or stable base Small-footprint loads Pallets needing continuous support Smooth continuous conveying, incline or decline sections, and movement of loads that require full-surface support Packaging, food and beverage support areas, clean production zones, carton-and-pallet transfer, and elevation changes Continuous support; relatively quiet operation; good traction; can accommodate smaller items on a pallet or irregular contact patterns Higher friction and belt wear; cleaning and tracking requirements; not always ideal for heavy accumulation without special design Belt material, sanitation requirements, incline angle, pallet bottom condition, belt tension, and product slip risk
Pallet Turntable Commonly 500–2,000 kg per pallet, depending on the rotating platform and conveyor interface Stable pallet footprint Rigid load unit Defined rotation clearance Changing pallet direction by 90° or 180° where floor space is limited or a layout requires a controlled turn Cross-docking, warehouse intersections, production cells, pallet inspection, and loading-area routing Efficient direction change; reduces the need for long curved conveyor sections; supports compact layouts Requires sufficient clearance; cycle time is affected by rotation; load must remain stable during turning Rotation angle, platform size, load center of gravity, turn cycle time, interface height, and safety guarding
Pallet Transfer Unit Approximately 500–2,500 kg per pallet, depending on lift, chain, roller, or belt mechanism Rigid pallets Consistent dimensions Stable load securing Moving pallets between parallel conveyor lines, lanes, workstations, or storage positions Production-line branching, warehouse buffers, sortation areas, and multi-lane pallet handling Provides flexible 90° transfers; maximizes floor-space use; can connect multiple conveyor lines More moving parts and controls; requires accurate positioning; transfer gaps must be managed carefully Transfer distance, pallet dimensions, positioning tolerance, cycle time, lifting stroke, and interaction with upstream controls
Pallet Lift or Vertical Conveyor Approximately 500–2,000 kg per pallet, based on lift configuration and safety design Stable unit load Uniform pallet dimensions Adequate load securing Moving pallets between floors or mezzanine levels while preserving a controlled, repeatable route Multi-level warehouses, manufacturing plants, distribution centers, and mezzanine storage systems Saves horizontal floor space; supports multi-floor workflows; can connect conveyors at different elevations Lower throughput than a continuous horizontal conveyor in many layouts; requires guarding, interlocks, and safe access control Vertical travel distance, cycle time, floor openings, fire protection, safety standards, pallet stability, and maintenance access
Pallet Shuttle Conveyor System Typically designed for pallet loads from approximately 500–1,500 kg, subject to shuttle and rack specifications Standardized pallets Uniform load dimensions Stable wrapped loads High-density storage and retrieval in deep-lane pallet racks with limited operator travel Cold storage, high-volume warehouses, buffer storage, and facilities requiring high storage density Improves storage density; reduces forklift travel inside lanes; suitable for repetitive storage and retrieval cycles Less flexible for mixed pallet dimensions; requires accurate pallet quality and rack tolerances; system controls are more complex FIFO or LIFO policy, lane depth, pallet quality, load stability, battery strategy, retrieval frequency, and fire-code requirements
Flexible or Expandable Pallet Conveyor Usually intended for lighter palletized loads; capacity depends strongly on the frame, wheel, or roller design Stable pallets Occasional-use loads Variable work areas Temporary loading, unloading, seasonal operations, and layouts that change frequently Small warehouses, vehicle loading points, project-based logistics, and overflow handling Quick to reposition; reduces fixed-installation cost; useful where conveyor routes change over time Generally lower capacity and durability than fixed systems; may provide limited accumulation and automation capability Maximum distributed load, floor condition, extension length, wheel or roller type, braking, and operator handling method
AGV or AMR Pallet Transport Interface Commonly 500–1,500 kg per vehicle or transfer cycle, based on vehicle configuration Stable unit load Defined pickup points Consistent pallet dimensions Flexible point-to-point movement between storage, production, staging, and shipping locations Smart factories, mixed-route warehouses, replenishment, kitting, and labor-reduction projects Highly flexible routing; scalable by adding vehicles; supports software-directed workflows and traceability Requires reliable navigation, traffic management, charging strategy, floor quality, and integration with warehouse or manufacturing software Vehicle payload, travel distance, traffic density, charging method, pickup accuracy, safety zoning, and system integration
Buyer selection rule: Confirm the actual pallet weight, pallet dimensions, bottom construction, load center of gravity, throughput, accumulation requirement, elevation changes, environmental conditions, and required safety standards before selecting a conveyor type.

Key Selection Criteria: Capacity, Safety, Layout, and Automation

2026 Top Pallet Conveyor Types for Global Buyers?

Capacity is the first filter, not the final decision. Specify pallets per hour, load weight, dimensions, and peak surges. A system moving 60 pallets hourly may need 90-pallet capacity during seasonal demand. Include accumulation space. Otherwise, motors run continuously and bottlenecks appear at dispatch.

Safety deserves measurable attention. The U.S. Bureau of Labor Statistics recorded 1,069 fatal work injuries in transportation and material-moving occupations during 2023. This figure is not conveyor-specific, but it shows why guarding, emergency stops, safe access, and operator training matter. Follow applicable local standards and recognized conveyor safety guidance. Test sensors with real pallet loads, not empty frames. Small gaps can create serious failure points.

Layout determines whether automation helps or complicates operations. Measure columns, doors, fire exits, floor strength, and maintenance clearance before choosing roller, chain, or turntable sections. Digital simulation is useful, but a spreadsheet can still lie. Walk the proposed route with operators. MHI’s 2024 Annual Industry Report found that 55% of respondents planned to increase supply-chain innovation investment, supporting stronger automation demand. Yet automation should match process stability. Start with barcode tracking, accumulation control, or selective routing when full integration is premature. A slower design may be safer, easier to service, and cheaper over ten years.

Global Purchasing Checklist: Standards, Costs, and Supplier Support

Global buyers comparing pallet roller, chain, and belt conveyors need more than a catalog price. Confirm pallet dimensions, maximum load, speed, accumulation method, and floor conditions. A roller conveyor may suit standard pallets, while chain conveyors handle awkward loads more reliably. Belt systems can reduce slipping but may increase maintenance needs.

Standards should be matched to the destination market, not copied from another project. Ask for safety calculations, guarding details, emergency-stop layouts, electrical documentation, and risk assessments. Request testing records and clear installation instructions. Requirements can vary by country and industry. The checklist is useful, but it is not perfect; local inspection practices may still change the final design.

Tips: Build a landed-cost sheet. Include equipment, controls, freight, customs charges, installation, training, spare parts, and commissioning. Then ask suppliers for a five-year maintenance estimate. A low quotation may hide costly transfers or limited support. Review the warranty carefully, especially for wear parts and control components. Require layout drawings before purchase, plus factory acceptance testing when practical. Confirm response times, remote troubleshooting, technician availability, software access, and replacement-part lead times. Small details matter. Supplier support often decides whether a conveyor remains productive after installation.

“Guardian has been a tremendous help in providing storage and distribution solutions for AIR Global. We came to Guardian with a need, and they quickly found a solution for us at a very reasonable price. Our business is very demanding, especially during busy periods, and Guardian has been flexible and able to accommodate all requests with less than 48 hours’ notice. April, our main contact, has been extremely helpful in making sure our orders are shipped on time and that our inventory is accurate. I highly recommend using Guardian and look forward to continuing our relationship for many years to come.”

Matt Buffington
Director of Supply and Operations
Americas

“The Guardian Logistics Team is responsive and helpful on a consistent basis.  This removes a tremendous amount of stress and gives us incentive to route cargo that will touch your dock. Thanks for all that you do!!!”

Charles Reel
Branch Manager
Scan Global Logistics

“I recommend with great confidence, Guardian Logistics Solutions and owner, Brent Smith to whomever needs top shelf deliveries including Last Mile, White Glove, Residential and Commercial.

I have known GLS since its inception. Guardian is always looking for the right answer to solve the customer’s problem. I can, without hesitation, recommend Guardian Logistics to any company that is looking for the best service in their coverage area. They will team with you to create a solution that suits your needs and ensure you are satisfied with the outcome.”

Steven T. Nelson

“I highly recommend Guardian Logistics Solutions. The professionalism and communications offered by the team, along with speediness, cost saving solutions and attitude is a testament to the fact that this is one of the most important partners you can have in the freight movement business.

The company offers exemplary service, they continuously exceed our expectations and that of the importers, they help us service, Guardian Logistics Solutions is the best solid business partner you should add to your company.”

Ubaldo Sierra
Maersk Customs Brokers
General Manager

“Guardian Logistic Solutions is one of those rare companies who under-promise-and-over-deliver EVERY single time!”

James Burke
Manager, Sales Team
OLIMP Warehousing

“I want to thank the team at Guardian for the excellent service we have received.
The shipments have been professionally handled and freight arrives timely and in good order at a fair price. Communication is a very important part of the handling and Guardian does a great job of communication through the delivery.”

Cheri Zetrouer
Access Worldwide
Customs Brokers & Freight Forwarders

“I am very lucky to have found Guardian Logistics to help with our freight needs.  Our business is a bit unique in that we only receive a shipment every 2-3 months and we have to stick to a very strict time schedule in order to unload the delivery.  We found it virtually impossible to consistently coordinate with logistics companies to have shipments arrive on time and when they were expected. After multiple frustrating scenarios, our broker introduced us to Guardian Logistics who handled all of our shipments recently to perfection. Our shipments have arrived on time, when expected, with friendly and helpful drivers.  We will only be using Guardian moving forward for all of our shipping and freight needs. I couldn’t recommend them strongly enough!”

Trey Conrad
Owner
Patriot Power Source

“We have been working with the Guardian company for several years now and I can say without a doubt that their entire team cares about the service they provide. Their personal interest in their customers’ success makes them a standout in the world of final mile delivery.

I highly recommend Guardian for anyone requiring outstanding services in warehousing and final mile delivery programs.”

Frank Ianucilli
Director of Final Mile Operations
Werner Enterprises

“At WeFixFreight.com, client satisfaction is our main priority.  We are proud to partner with the top notch team at Guardian to bring our customers nothing but the best service when it comes to freight reworks, cross docking services, and final mile delivery.”

Bill Carlin
CEO
WeFixFreight.Com

“The Guardian Logistics staff has always been exceptional, and these days, with all the competition out there, it’s the service that matters. We appreciate all they do and look forward to continuing our business with GLS.”

Cathy Avolio
Ocean Import Manager
Mallory Alexander Int'l Logistics (NY), LLC
Back To Top