Skip to content

What Is an Aluminum Extrusion Die Used For?

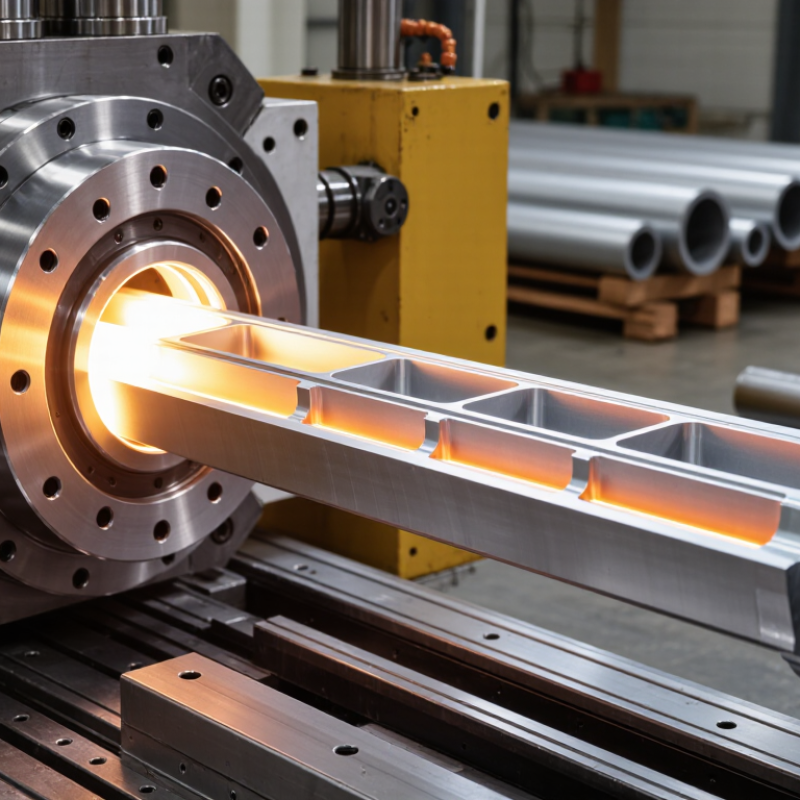
An Aluminum Extrusion Die is a precision tool that shapes heated aluminum as a press pushes it through a formed opening. The result may be a simple angle, a window frame, or a hollow profile with narrow internal channels. The die does more than define the outline. Its bearing surfaces help control metal flow, while its strength and temperature stability affect dimensions, surface finish, and service life. Small details matter. A slight imbalance in flow can leave one side of a profile thicker or cause it to bend after leaving the press.

Demand for aluminum gives this tooling a significant industrial role. The International Aluminium Institute reported roughly 70.6 million tonnes of global primary aluminum production in 2023. That figure covers primary metal, not extrusion alone, so it should not be mistaken for die-market size. Still, it shows the scale of the material supply behind products used in transport, construction, electronics, and renewable-energy equipment. The U.S. Geological Survey’s annual mineral summaries provide another authoritative reference for global aluminum production and supply.

Understanding what an Aluminum Extrusion Die is used for means looking beyond the opening in the tool. Engineers consider alloy, profile geometry, press capacity, cooling, and required tolerances before choosing a die design. A complex hollow section may need a porthole die; a solid shape may use a simpler flat die. There is no universal best option. Even a carefully designed die can require adjustment after trial runs, and that part is easy to underestimate. The sections below explain how dies work, where they are used, and which design factors influence results.
What Is an Aluminum Extrusion Die Used For?

What an Aluminum Extrusion Die Is

What Is an Aluminum Extrusion Die Used For?

What an Aluminum Extrusion Die Is

An aluminum extrusion die is a hardened steel tool with a precisely shaped opening. It forms heated aluminum into a continuous profile. The profile may become a window frame, heat sink, rail, tube, or structural section.

The die opening controls the product’s outside shape. Internal bridges or mandrels can create hollow spaces. A thicker bearing area slows metal flow. This helps different sections leave the die at similar speeds. Even small design changes can affect wall thickness, surface finish, and dimensional accuracy.

In practical production, the billet is heated before a press pushes it through the die. Pressure forces the aluminum to follow the opening. The emerging profile is then cooled, stretched, cut, and inspected. It is not a mold in the usual sense. The die does not create separate pieces; it creates a long, consistent shape.

In practice, the first trial can disappoint. Uneven flow may twist the profile or leave one wall too thin. Engineers may adjust the bearing lengths, press speed, or billet temperature. These corrections require measurement, not guesswork. Die wear also matters. Scratches, chipped edges, or poor cleaning can mark every meter of extrusion. A reliable process therefore includes dimensional checks, surface inspection, and scheduled die maintenance. Some profiles remain difficult, even when the drawings look perfect.

How a Die Shapes Heated Aluminum

An aluminum extrusion die is a hardened steel tool with an opening that gives softened aluminum its cross-sectional shape. A press pushes a heated billet through this opening, much like squeezing paste through a patterned nozzle, though the forces and temperatures are far greater. The metal emerges as a continuous profile, such as a channel, tube, or window frame.

The opening is only part of the story. Its narrow shaping surfaces, called bearings, help guide metal flow and influence the profile’s dimensions. If metal moves unevenly, one side may leave the die faster than another. The result can twist or vary in thickness. For hollow shapes, a mandrel forms the inner space while the surrounding die defines the outside. It is a demanding balance.

After exiting the die, the hot profile is cooled and often straightened or stretched to reduce distortion. Operators monitor temperature, press speed, and dimensions because small changes can affect the finished shape. Even a carefully designed die may need adjustment after a trial run; real aluminum does not always flow exactly as calculations predict. That uncertainty is worth respecting. The die shapes the metal, but process control helps make each length consistent.

Key Functions of an Extrusion Die

An aluminum extrusion die shapes heated aluminum as it passes through a precisely formed opening. Its key function is to control the profile’s cross-section, creating features such as channels, ribs, or hollow spaces. The die also guides metal flow. Balanced flow helps keep walls even and dimensions consistent along the finished length. Small design errors can cause uneven surfaces or weak, thin sections. Die design is not just about the opening; bearing lengths, metal temperature, and press speed also affect the result.

A die must withstand pressure and heat while maintaining its geometry over repeated production cycles. Its construction and condition influence surface finish, tolerances, and output rate. For hollow profiles, bridge or porthole features divide and rejoin the aluminum under pressure. The weld quality depends on process control, not die shape alone. In practice, even a well-made die may need adjustment after trial runs. That part is easy to underestimate.

Tips: Match the die design to the profile’s wall thickness and intended use. Avoid sudden, deep changes in section when possible; they can make metal flow harder to balance. Check sample extrusions for twists, rough patches, and dimensional drift. A simple measurement log can reveal patterns. It will not fix everything, but it helps guide useful die changes.

Common Profiles and Products Made with Dies

Aluminum extrusion dies shape heated aluminum into consistent cross-sections. Common profiles include round tubes, square channels, angles, T-slots, and hollow sections. These shapes appear in window frames, door tracks, curtain-wall framing, and machine guards. A narrow groove can hold a gasket; a hollow chamber may improve stiffness without adding much weight. The exact profile depends on its intended load, fit, and finish.

Dies also produce components for equipment and everyday products. Heat sinks use closely spaced fins to release heat. Conveyor rails, solar-panel frames, furniture parts, and vehicle trim often rely on extruded sections. Some profiles are simple and sturdy; others include several cavities or thin walls. Those details can reduce material use, but they may make die design and production more demanding. A profile that looks easy on paper can prove difficult to extrude evenly.

Tips: Share a clear cross-section drawing and specify critical dimensions, wall thickness, and alloy. Ask whether thin features or sharp corners need adjustment. Small changes can improve metal flow and reduce distortion. Still, the ideal shape is not always obvious until samples are measured and tested.

Factors That Influence Die Design and Selection

An aluminum extrusion die shapes heated billet as pressure pushes metal through its opening. Its design affects profile accuracy, surface finish, production speed, and tool life. The right die is not simply the one that matches a drawing. Engineers also consider alloy, billet temperature, press capacity, and the profile’s thinnest walls.

Geometry matters. A wide, thin section may need carefully balanced metal flow to prevent twisting or uneven thickness. Hollow profiles require bridges and mandrels, which add complexity and can leave visible weld lines. Die steel, bearing length, and cooling conditions also influence performance. Small changes count. A longer bearing can slow metal flow in one area, but may increase press load and heat.

Demand adds pressure to improve tooling. The International Aluminium Institute’s 2023 Global Aluminium Cycle report projected global aluminium demand could rise from 86.2 million tonnes in 2020 to 119.5 million tonnes by 2030. That growth makes efficient die design more important, though demand forecasts cannot specify a die’s exact geometry. In practice, designers rely on simulation, trial runs, and measured samples. They check dimensions, corner fill, and surface marks after extrusion. Not every first trial works. That is useful feedback, but it also shows why material data and realistic tolerances matter. A feature that looks simple on a screen may be difficult to fill consistently on a press.

What Is an Aluminum Extrusion Die Used For? — Factors That Influence Die Design and Selection

Die Type or Feature Typical Use Key Design Considerations Selection Factors
Solid die Produces profiles without enclosed hollow spaces, such as bars, angles, channels, and solid rails. Opening shape, bearing lengths, metal flow balance, die strength, and profile tolerances. Profile geometry, alloy, required dimensions, production volume, and press capacity.
Hollow die Forms profiles with enclosed cavities, such as tubes and multi-chamber sections. Mandrel support, weld-chamber design, metal flow around the mandrel, and seam quality. Number and size of cavities, wall thickness, dimensional accuracy, alloy, and extrusion pressure.
Semihollow die Produces profiles with partially enclosed openings, including narrow slots and complex channels. Opening size relative to profile dimensions, tongue strength, bearing design, and risk of die deflection. Slot geometry, minimum wall thickness, profile complexity, and practical press limits.
Profile cross-section Defines the shape and functional features of the extruded product. Uniform wall thickness, corner radii, symmetry, rib placement, and avoidance of abrupt section changes. Part function, assembly requirements, finishing needs, material use, and achievable tolerances.
Wall thickness and section complexity Influence how easily metal fills thin, thick, and intricate areas of the profile. Flow balance between regions, local die strength, bearing lengths, and the risk of incomplete filling. Minimum wall thickness, thickness variation, alloy flow characteristics, and extrusion ratio.
Bearing lengths Help control the speed and uniformity of metal exiting different parts of the die. Different regions may require different bearing lengths to compensate for uneven flow resistance. Profile shape, metal-flow behavior, dimensional requirements, and trial-extrusion results.
Alloy and temper Determine the material’s forming behavior and the processing conditions needed for extrusion. Alloys differ in flow stress, extrusion temperature range, surface response, and cooling behavior. Strength, corrosion resistance, surface finish, downstream processing, and intended application.
Press and billet capacity Set practical limits for the size and complexity of an extrusion job. Die diameter, billet size, extrusion ratio, operating pressure, and available container dimensions. Press force, billet dimensions, profile perimeter, alloy, and expected production rate.
Dimensional tolerances Specify the acceptable variation in profile dimensions and shape. Die deflection, thermal expansion, metal-flow variation, and profile distortion during cooling. Fit and function, applicable tolerance requirements, inspection method, and production consistency.
Production volume and die life Influence the required durability, maintenance plan, and overall tooling approach. Die steel and heat treatment, operating conditions, wear-prone areas, and repairability. Expected run length, complexity of replacement, maintenance costs, and repeat-order needs.

“Guardian has been a tremendous help in providing storage and distribution solutions for AIR Global. We came to Guardian with a need, and they quickly found a solution for us at a very reasonable price. Our business is very demanding, especially during busy periods, and Guardian has been flexible and able to accommodate all requests with less than 48 hours’ notice. April, our main contact, has been extremely helpful in making sure our orders are shipped on time and that our inventory is accurate. I highly recommend using Guardian and look forward to continuing our relationship for many years to come.”

Matt Buffington
Director of Supply and Operations
Americas

“The Guardian Logistics Team is responsive and helpful on a consistent basis.  This removes a tremendous amount of stress and gives us incentive to route cargo that will touch your dock. Thanks for all that you do!!!”

Charles Reel
Branch Manager
Scan Global Logistics

“I recommend with great confidence, Guardian Logistics Solutions and owner, Brent Smith to whomever needs top shelf deliveries including Last Mile, White Glove, Residential and Commercial.

I have known GLS since its inception. Guardian is always looking for the right answer to solve the customer’s problem. I can, without hesitation, recommend Guardian Logistics to any company that is looking for the best service in their coverage area. They will team with you to create a solution that suits your needs and ensure you are satisfied with the outcome.”

Steven T. Nelson

“I highly recommend Guardian Logistics Solutions. The professionalism and communications offered by the team, along with speediness, cost saving solutions and attitude is a testament to the fact that this is one of the most important partners you can have in the freight movement business.

The company offers exemplary service, they continuously exceed our expectations and that of the importers, they help us service, Guardian Logistics Solutions is the best solid business partner you should add to your company.”

Ubaldo Sierra
Maersk Customs Brokers
General Manager

“Guardian Logistic Solutions is one of those rare companies who under-promise-and-over-deliver EVERY single time!”

James Burke
Manager, Sales Team
OLIMP Warehousing

“I want to thank the team at Guardian for the excellent service we have received.
The shipments have been professionally handled and freight arrives timely and in good order at a fair price. Communication is a very important part of the handling and Guardian does a great job of communication through the delivery.”

Cheri Zetrouer
Access Worldwide
Customs Brokers & Freight Forwarders

“I am very lucky to have found Guardian Logistics to help with our freight needs.  Our business is a bit unique in that we only receive a shipment every 2-3 months and we have to stick to a very strict time schedule in order to unload the delivery.  We found it virtually impossible to consistently coordinate with logistics companies to have shipments arrive on time and when they were expected. After multiple frustrating scenarios, our broker introduced us to Guardian Logistics who handled all of our shipments recently to perfection. Our shipments have arrived on time, when expected, with friendly and helpful drivers.  We will only be using Guardian moving forward for all of our shipping and freight needs. I couldn’t recommend them strongly enough!”

Trey Conrad
Owner
Patriot Power Source

“We have been working with the Guardian company for several years now and I can say without a doubt that their entire team cares about the service they provide. Their personal interest in their customers’ success makes them a standout in the world of final mile delivery.

I highly recommend Guardian for anyone requiring outstanding services in warehousing and final mile delivery programs.”

Frank Ianucilli
Director of Final Mile Operations
Werner Enterprises

“At WeFixFreight.com, client satisfaction is our main priority.  We are proud to partner with the top notch team at Guardian to bring our customers nothing but the best service when it comes to freight reworks, cross docking services, and final mile delivery.”

Bill Carlin
CEO
WeFixFreight.Com

“The Guardian Logistics staff has always been exceptional, and these days, with all the competition out there, it’s the service that matters. We appreciate all they do and look forward to continuing our business with GLS.”

Cathy Avolio
Ocean Import Manager
Mallory Alexander Int'l Logistics (NY), LLC
Back To Top